Deep-Hole Boring & Honing
Boring, skiving and roller burnishing, and honing of cylinder bores to tolerance and finish.
Getting a bore round, straight and finished
Three processes overlap here. Boring establishes the hole, skiving and roller burnishing produce a finished bore quickly on long tube, and honing gives the finest control of roundness, cylindricity and surface finish. Which route is right depends on length-to-bore ratio, wall thickness and the seal package.
For a reference point, an established North American tube specialist publishes honing capability of 1/2 inch to 75 inch bore up to 80 feet in length, with a standard finish of 10 to 20 microinch and 4 to 6 microinch achievable. Our own figures belong in the table below and must be measured, not aspired to.
Capability
| CAPABILITY | ORISE VALUE |
|---|---|
| Boring: bore range | Ø40 to Ø400 mm |
| Boring: maximum depth | 8000 mm |
| Honing: bore range | Ø40 to Ø500 mm |
| Honing: maximum length | 8000 mm |
| Honing: repeatable Ra | Ra 0.2 to 0.8 µm, Ra 0.4 µm standard |
| Honing: ovality held | Not more than half the applicable ID tolerance band |
| Honing: bore tolerance held | H8 standard, H7 on enquiry |
| Skiving and roller burnishing: bore range | Ø40 to Ø400 mm |
| Skiving and roller burnishing: maximum length | 7000 mm |
| Skiving and roller burnishing: Ra | Ra 0.2 to 0.4 µm |
| Bore straightness held | 0.5 mm/m honed · 0.2 to 0.3 mm/m skived and roller burnished |
| Maximum part weight | 1200 kg |
| Bore measurement method | Two-point and three-point bore gauges with setting rings, CMM for form and position |
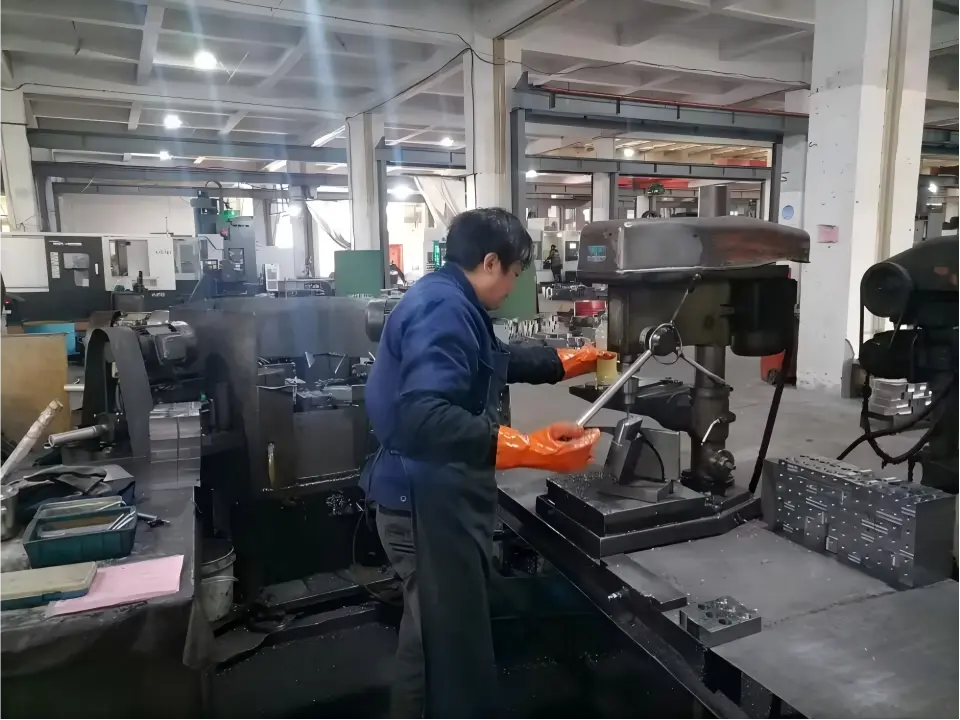
Measurement is the hard part. A long bore is easy to hone and difficult to prove. State on the drawing how the bore is to be measured and at how many positions, and the inspection record will match your incoming check rather than argue with it.
Send the drawing
Quotation within 48 hours of a complete drawing package.