Welding
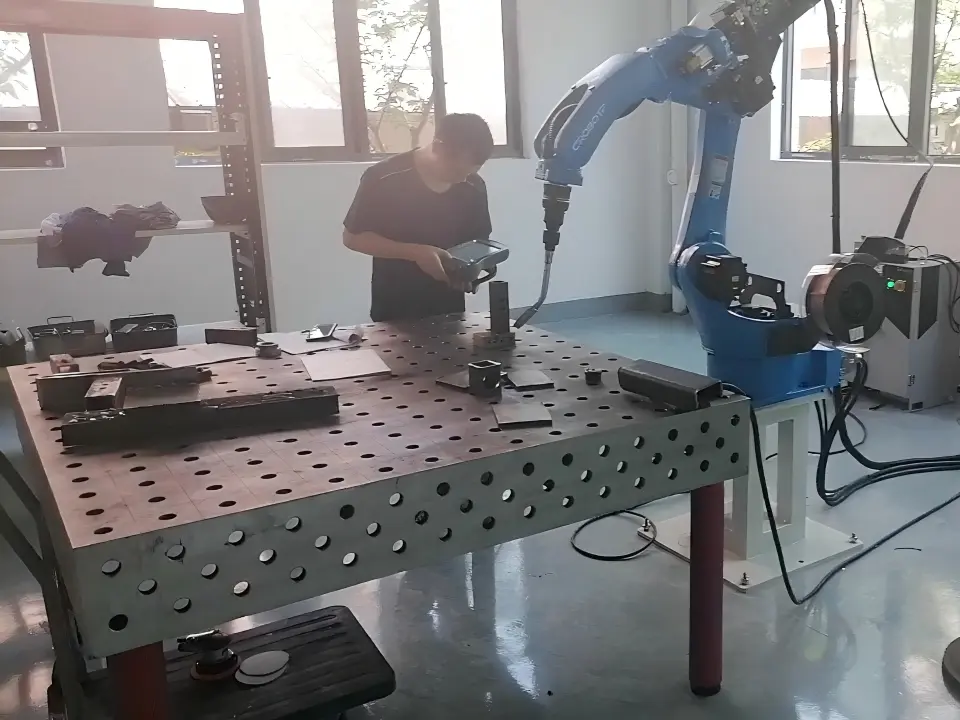
MIG / MAG and submerged arc welding of cylinder sub-assemblies, with welder qualification records retained.
Welding, then machining
Welded cylinder work is only as good as the sequence. Weld, stress relieve where required, then establish the machining datum and cut. Any other order produces an assembly that measures correctly part by part and is out of tolerance as a whole.
Welder qualification records exist per welder and per procedure and are available at the quotation stage rather than only during an audit.
Capability
| CAPABILITY | ORISE VALUE |
|---|---|
| Processes available | MIG / MAG · submerged arc · TIG |
| Automation | CNC seam welding stations for tube-to-head and tube-to-base joints |
| Maximum assembly length | 6000 mm |
| Maximum assembly weight | 3000 kg |
| Crane capacity in the welding bay | 10 t |
| Welder qualification | Records held per welder and per procedure, copies supplied with the first article |
| Welding procedure specifications | Held per joint type and issued with the first article on request |
| Welding quality system | Covered by the ISO 9001 system. ISO 3834 is not held and is not claimed |
| Rail sector welding | EN 15085 is not held. Rail work requiring it should go to a certified shop |
| Stress relief furnace | 550 to 650 °C, parts up to 6000 mm |
| NDT available | Visual, magnetic particle and ultrasonic in house · radiography through a qualified partner |
| Post-weld machining in one set-up | Yes. Datum re-established after welding |
Send the drawing
Quotation within 48 hours of a complete drawing package.