Forging & Die Design
Closed-die forging of cylinder and breaker components, with tool and die design and manufacture in house.
Forging and tooling under one roof
Forged blanks give critical cylinder and breaker parts a continuous grain flow and a fatigue strength that machined bar stock cannot reach. Designing and cutting the dies in house lets ORise control lead time, die life and the machining allowance left for finish machining.
Where the drawing permits a forged form, the part is quoted as forged and machined rather than machined from solid. The decision is made on the drawing, not on what is easiest to load into a lathe.
Capability
| CAPABILITY | ORISE VALUE |
|---|---|
| Forging processes | Closed-die and open-die forging |
| Closed-die press capacity | Up to 1600 t on the main line · larger by partner forge |
| Open-die hammer capacity | Up to 5 t per piece |
| Forged weight range | 0.5 to 80 kg typical per piece · to drawing |
| Materials forged | Carbon and alloy steel: 20#, 35#, 45#, 40Cr, 42CrMo (AISI 1045 / 5140 / 4140), 20MnV |
| Die material | H13 / 1.2344 hot-work tool steel, hardened and tempered |
| Die design | In-house CAD/CAM, 3D modelling and forging simulation |
| Die life | 8,000 to 30,000 shots typical for H13 dies, to drawing |
| Machining allowance, as forged | 2 to 4 mm per side typical, to drawing |
| As-forged tolerance | ±1.5 mm typical; finish machining required for final dimensions |
| Forging ratio (grain flow) | Minimum 3:1 where the drawing specifies |
| Post-forge heat treatment | Normalising or quench and temper, hardness recorded per batch |
| Inspection | UT and MT available for critical forgings; hardness and dimensions per batch |
| Forging in house or by partner | In house for the standard range; partner forge for very large or special alloys |
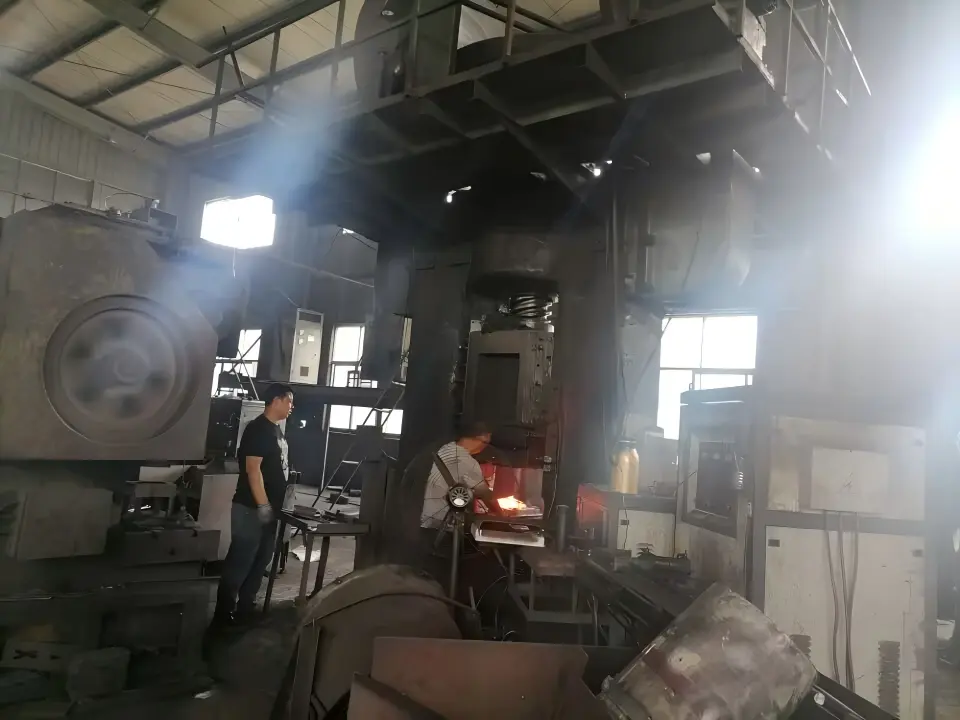
Say whether forging is in house. A supplier who forges and machines in one plant can trace a part from billet to finished dimension on a single record. One who subcontracts forging should name the forge and the material certificate flow.
Lead time lever. In-house tool and die design is the single biggest lever on new-part lead time. Buyers asking for a prototype in weeks, not months, are really asking whether the die can be cut on site.
Send the drawing
Quotation within 48 hours of a complete drawing package.